Case studies
CNC Machining Case Studies
Real programs, real constraints — how parts that were hard to make got made, measured and delivered.
Aerospace
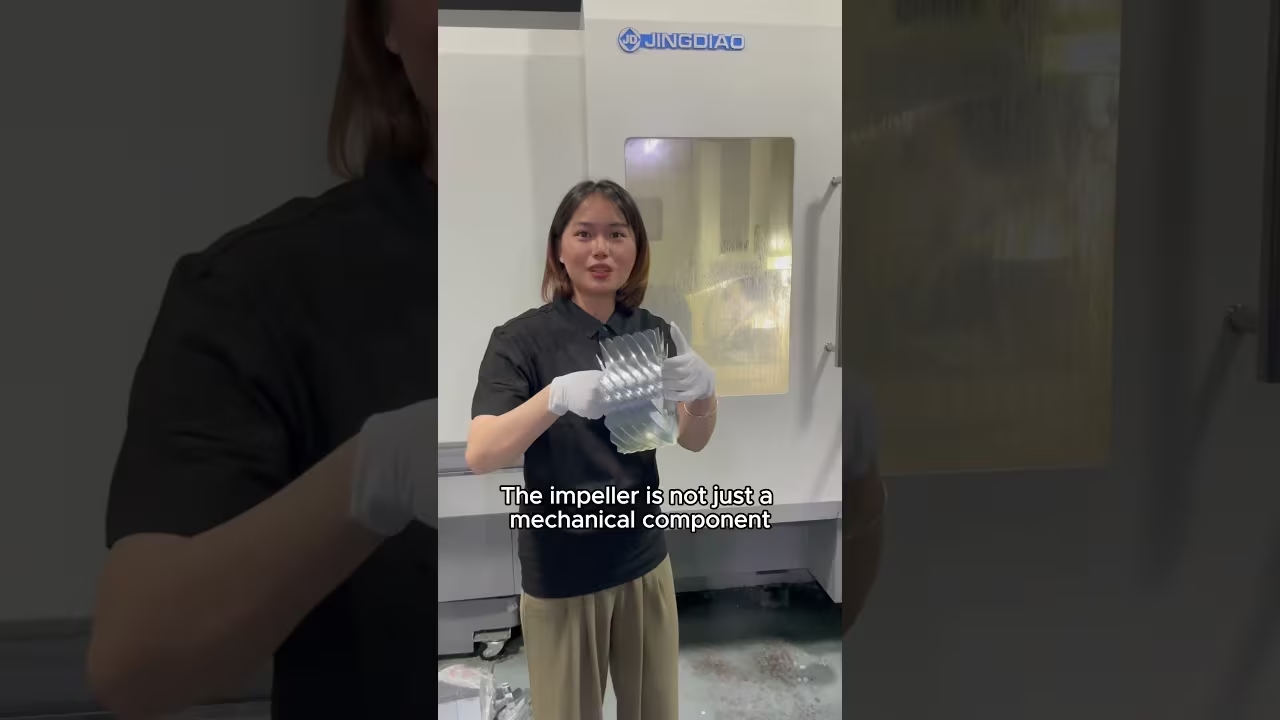
Thin-walled titanium impeller, 0.008 mm profile
The challenge: a 240 mm impeller with 2.2 mm blades and a 0.008 mm profile tolerance. Previous suppliers fought chatter and deflection, and delivered with blend marks on the flow surfaces.
What we did: five-axis simultaneous toolpaths with adaptive stock removal, a purpose-built expanding mandrel for blade support, and a finishing strategy that kept the tool normal to the swept surface through the whole blade height. Cut data was validated on a partial test blank before touching the real part.
Result: first article approved at 0.006 mm profile, three-week delivery, zero rework. The mandrel and program now run as a repeatable production route.
- Profile: 0.006 mm on a 0.008 mm requirement
- Surface finish: Ra 0.8 μm on flow surfaces
- Lead time: 3 weeks from drawing release
Automotive & EV
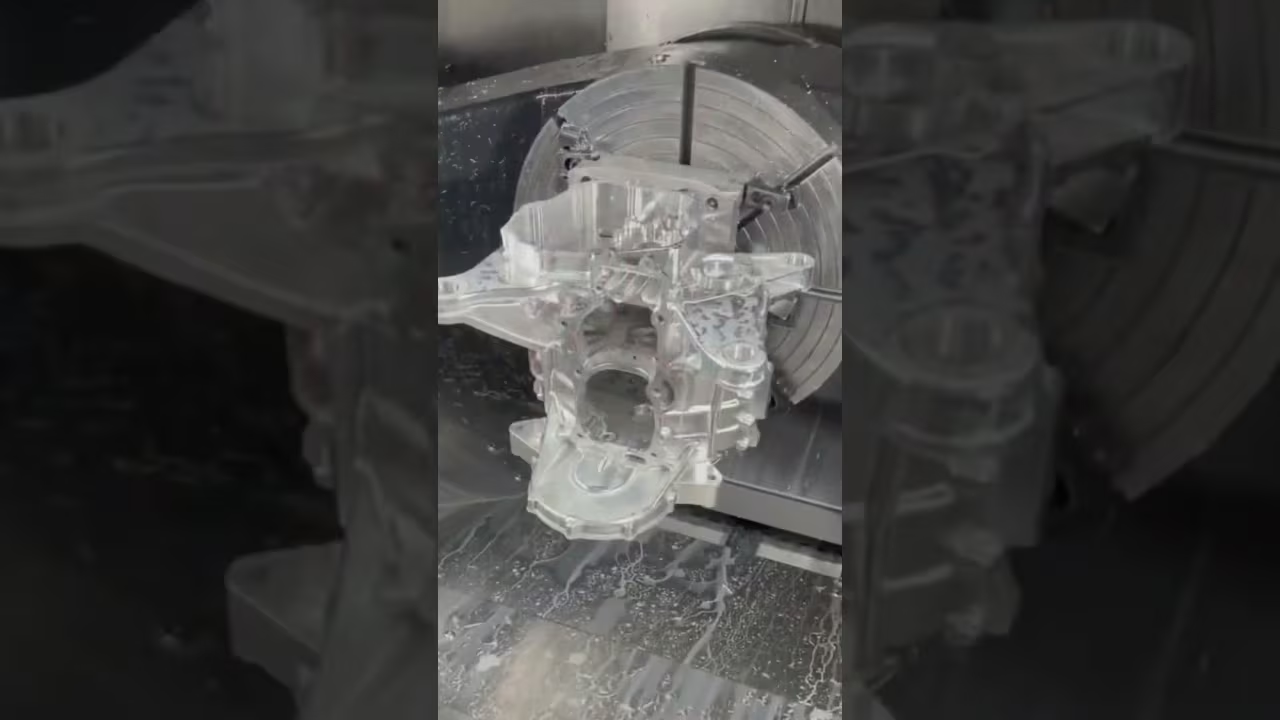
Engine housing: prototype to 2,000 pcs/month
The challenge: an OEM needed functional prototypes in three weeks — and a credible path to 2,000 pieces per month with IATF 16949 documentation, without re-doing the process from scratch.
What we did: prototype and production cells designed together: same datums, same fixtures, same probing. Machined interfaces held to ±0.02 mm with in-process verification, and PPAP documentation was built during, not after, the ramp.
Result: prototypes approved on schedule; production cell running with in-process probing and 400-piece weekly batches; scrap rate under 0.5% across the first six months.
- Prototype: 3 weeks (5-axis machined)
- Production: 2,000 pcs/month, IATF 16949 documentation
- Scrap rate: <0.5% (first 6 months)
Humanoid Robotics
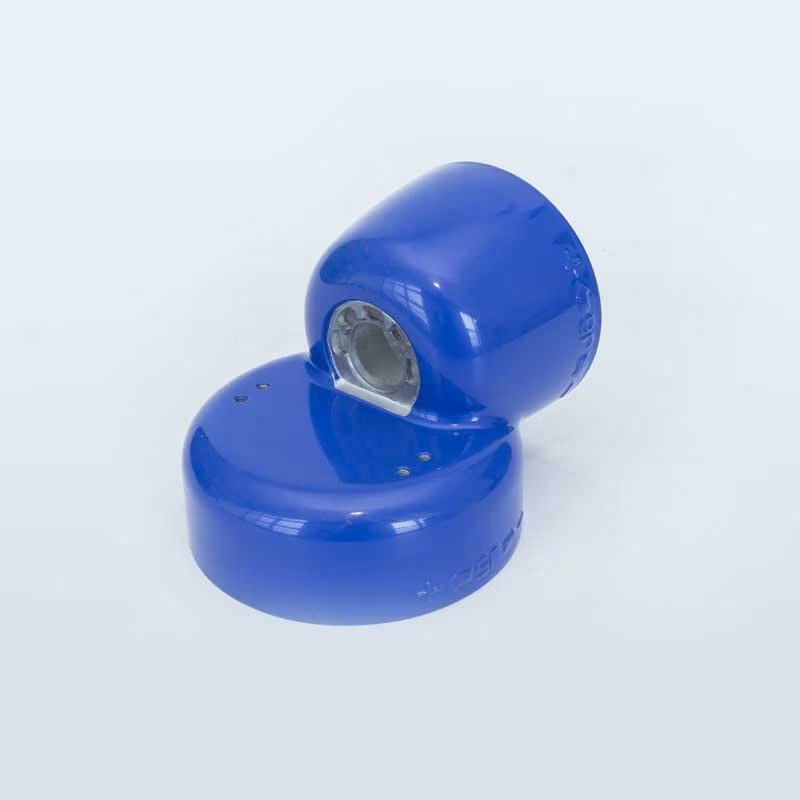
Robot actuator housings, ±0.01 mm on every unit
The challenge: a robotics company needed actuator housings with bearing bores that had to interchange without shimming — 500 units per month, five housing variants, delivered as kits.
What we did: dedicated fixtures per variant, mill-turn processing for concentricity, and SPC monitoring on the bore diameter with monthly capability reports to the customer.
Result: interchangeability achieved on every shipment; the customer eliminated a shim-fitting step in assembly and later added two more variants to the program.
- Concentricity: within 0.01 mm, Cpk > 1.33 on bore diameter
- 500 units/month across 5 variants, kit delivery
Your part could be next
Send the drawing — we will tell you exactly how we would make it, what it will cost, and how long it takes.