Services
Metal Die Casting Services
Aluminum and zinc die casting with tooling, machining and finishing in-house — a stable route to complex housings at volume.
Casting and machining from one supplier
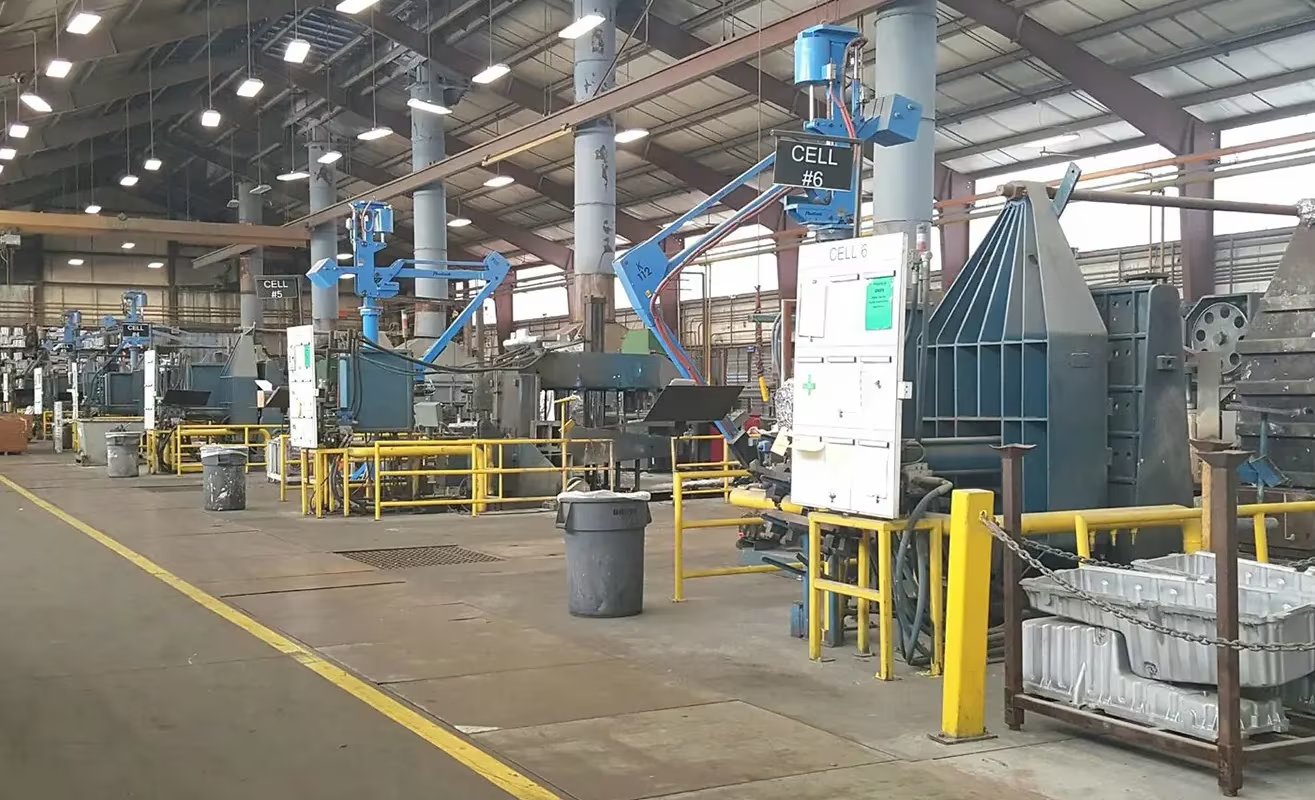
Die casting economics depend on the whole chain: tool design, casting parameters, machining datums and finishing all interact. Because our tooling shop, casting cell and CNC department sit in one building, we control that chain end to end — and when a casting needs a design tweak, it happens before the tool is cut, not after.
A typical program looks like this: DFM and mold-flow review, tool manufacture, first-article approval with CT/CMM reports, then cast, de-gate, machine, finish and ship — with the same part ever leaving our system.
- Aluminum (ADC12 / A380) and zinc (Zamak 3 / 5) casting
- Tool design, manufacture and maintenance in-house
- Machining fixtures and CNC finishing planned with the tool
- First-article inspection with dimensional and porosity reports
- Powder coating, painting, anodizing and assembly to finish
Specifications
Die casting at a glance
| Parameter | Capability |
|---|---|
| Processes | Hot-chamber (zinc) and cold-chamber (aluminum) die casting |
| Alloys | ADC12, A380, ADC6 (aluminum); Zamak 3, Zamak 5 (zinc) |
| Part size | From a few grams up to approx. 10 kg cast weight |
| Tolerances | As-cast per NADCA practice; ±0.02 mm achievable on machined interfaces |
| Tooling | Designed and maintained in-house; 15–45 day tool lead time typical |
| Secondary ops | De-gating, tumbling, CNC machining, drilling, tapping, impregnation |
| Finishes | Powder coating, painting, shot blasting, vibratory polishing, anodizing (aluminum) |
Typical annual volumes: 5,000–500,000 pcs. For lower volumes we will quote casting alternatives (sand cast, gravity cast, or machined-from-solid) side by side.
Typical parts
What we cast
- Lighting housings
- Motor end-bells
- Robot joint covers
- EV brackets & carriers
- Communication enclosures
- Pump housings
- Instrument cases
- Lock & hardware bodies